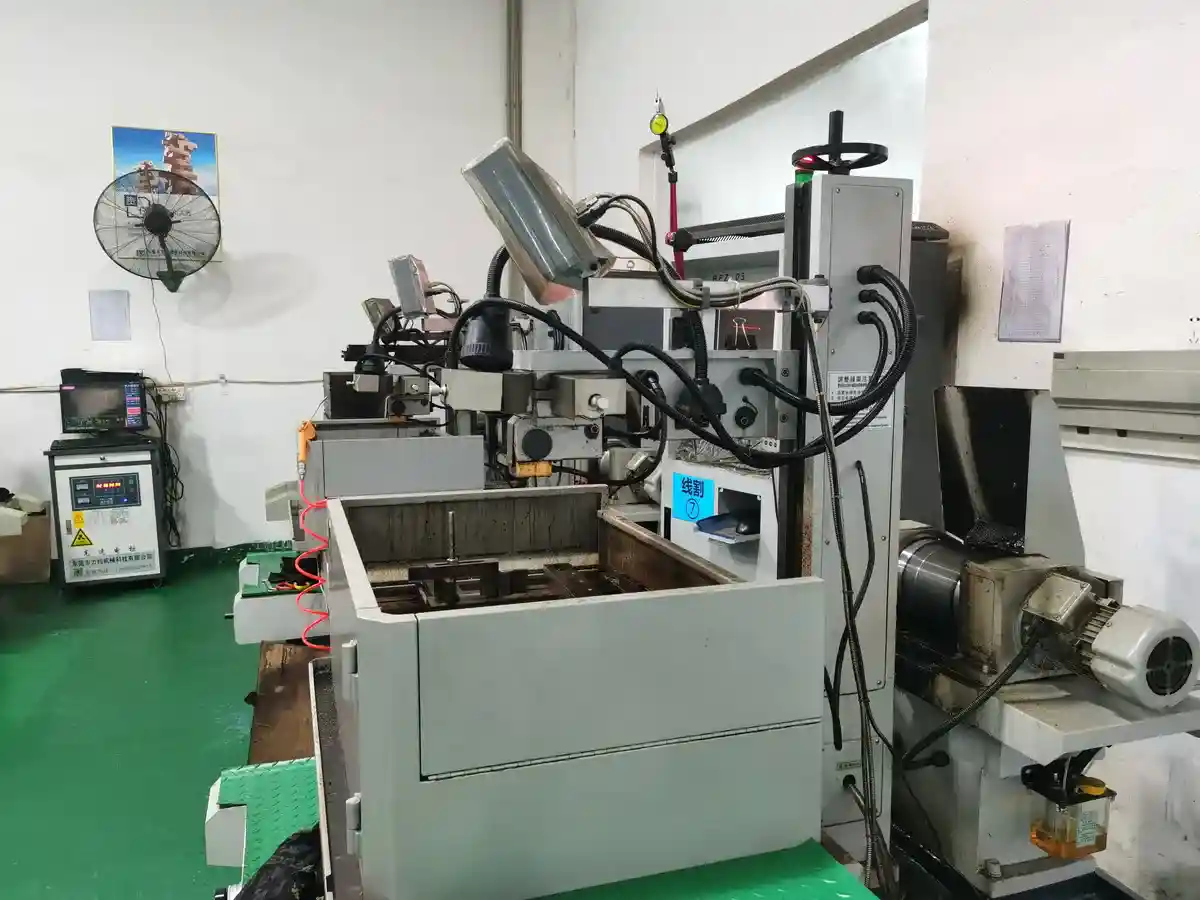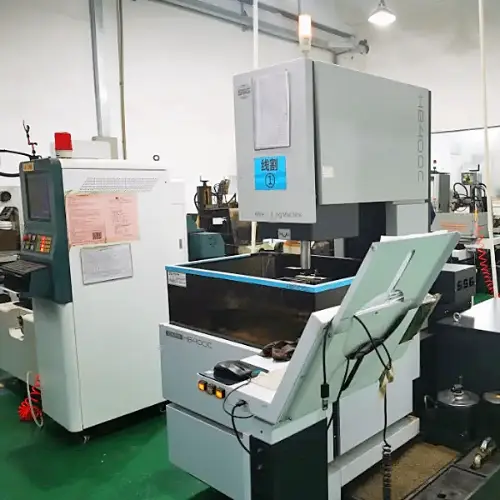
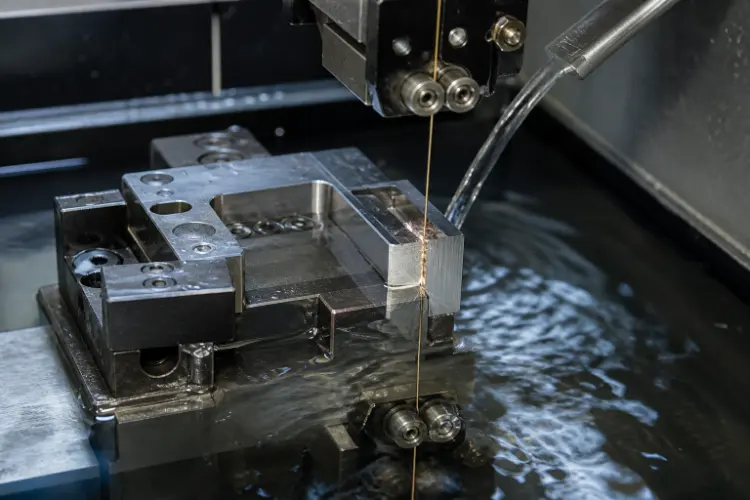
Precision Wire EDM Machining
Controlled Wire EDM machining for molds, tooling, and complex components made from electrically conductive materials.
Materials for Wire EDM
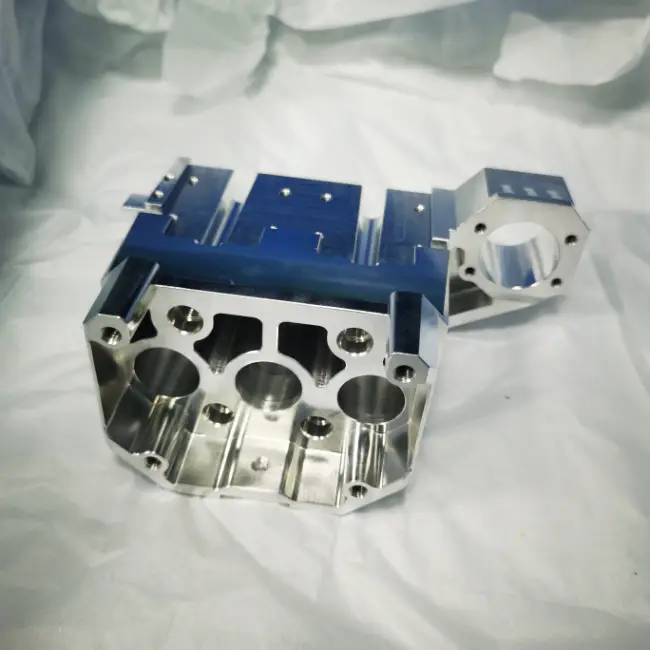
Aluminum
Aluminum can be wire-cut into complex profiles with minimal mechanical distortion. Cutting speed and surface finish depend on alloy, thickness, flushing, and discharge settings.
View material details
- Characteristics
- Lightweight, corrosion-resistant, and thermally conductive, with performance that varies by alloy and temper.
- Typical Wire-EDM Parts
- Aerospace brackets, fixture plates, mold components, precision slots, and lightweight structural profiles.
- Machining Notes
- Use alloy-specific discharge settings and stable flushing. Control debris evacuation, wire offset, electrochemical staining, and corner accuracy.

Stainless Steel
Wire EDM produces accurate slots and profiles in stainless steel, including hardened conditions. Settings must balance cutting rate, surface roughness, and dimensional control.
View material details
- Characteristics
- High strength, corrosion resistance, heat resistance, and good dimensional stability.
- Typical Wire-EDM Parts
- Medical tooling, valve components, die inserts, precision shims, guides, and fine-profile instrument parts.
- Machining Notes
- Select pulse and trim-cut settings according to thickness and finish requirements. Clean and dry parts after cutting, and specify passivation when required.
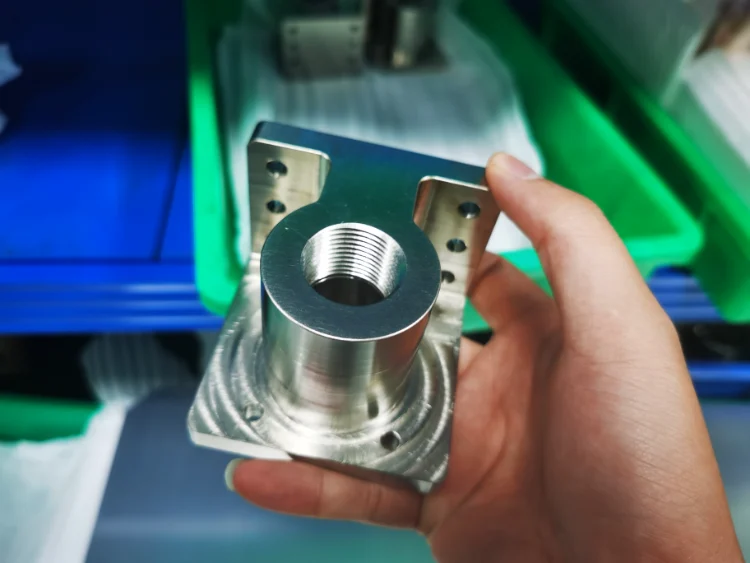
Tool Steel & Cemented Carbide
Hardened tool steels are well suited to Wire EDM. Cemented carbide requires grade-specific settings to control microcracking, binder corrosion, and edge damage.
View material details
- Characteristics
- Tool steels provide hardness and toughness; cemented carbides combine hard WC particles with a metallic binder for high wear resistance.
- Typical Wire-EDM Parts
- Punches, dies, mold inserts, gear profiles, cutting tools, wear plates, and precision carbide components.
- Machining Notes
- For carbide, confirm grade and binder content. Use low-energy trim passes, controlled flushing, corrosion management, and supported edges.
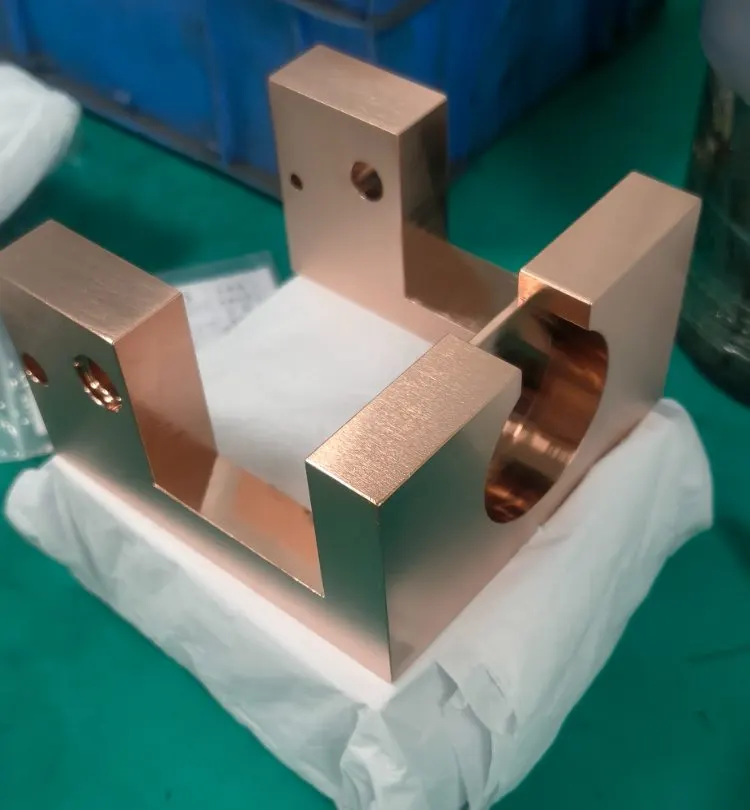
Copper & Brass
Copper and brass are Wire-EDM compatible, but high thermal conductivity requires tuned discharge energy and stable flushing for consistent accuracy and surface quality.
View material details
- Characteristics
- Excellent electrical and thermal conductivity, good corrosion resistance, and grade-dependent softness.
- Typical Wire-EDM Parts
- Electrodes, terminals, connectors, conductive fittings, cooling components, and precision instrument parts.
- Machining Notes
- Support soft workpieces carefully and control wire offset, flushing pressure, heat dissipation, surface marking, and post-cut oxidation.
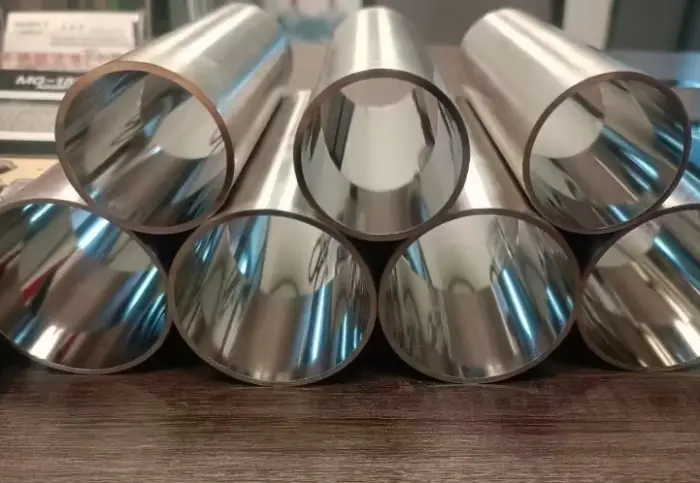
Titanium & High-Temperature Alloys
Wire EDM cuts titanium and nickel-based high-temperature alloys without mechanical force. Multiple trim passes may be required to control the recast layer and surface integrity.
View material details
- Characteristics
- High specific strength, corrosion resistance, heat resistance, and dependable performance in demanding environments.
- Typical Wire-EDM Parts
- Aerospace brackets, turbine components, medical parts, heat-resistant inserts, and complex high-strength profiles.
- Machining Notes
- For fatigue-sensitive, medical, or aerospace parts, specify recast-layer limits and whether polishing, chemical cleaning, or other post-processing is required.
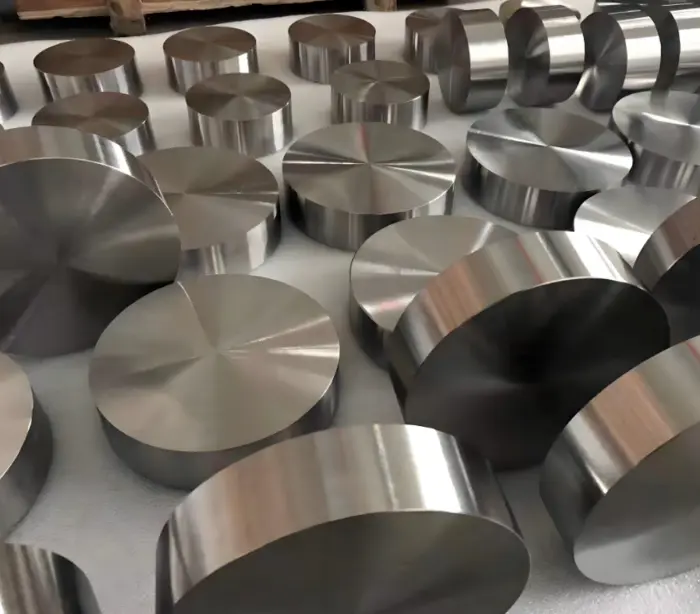
Tungsten & Molybdenum
Wire EDM produces precise profiles in these refractory metals without mechanical cutting force, although cutting speed is typically lower and material-specific settings are required.
View material details
- Characteristics
- Very high melting points, good high-temperature strength, electrical conductivity, and demanding conventional machinability.
- Typical Wire-EDM Parts
- High-temperature inserts, electrodes, precision apertures, semiconductor components, and refractory-metal profiles.
- Machining Notes
- Use grade-specific parameters, controlled flushing, and multiple trim passes to manage cutting stability, edge quality, and surface integrity.
Graphite, conductive ceramics, and conductive composites are reviewed separately. Conventional Wire EDM requires sufficient electrical conductivity; exact grade, porosity, thickness, and edge requirements must be confirmed before quoting.
4 Steps to a Controlled Cut
Programming, wire selection, discharge settings, dielectric control, and inspection are planned together.
Drawing review
Confirm datum, profile, start hole, taper, tolerance, roughness, and thickness.
Programming & setup
Select wire diameter, tension, offset, pulse settings, and dielectric conditions.
Rough and skim cuts
Balance cutting time, dimensional control, and required surface finish.
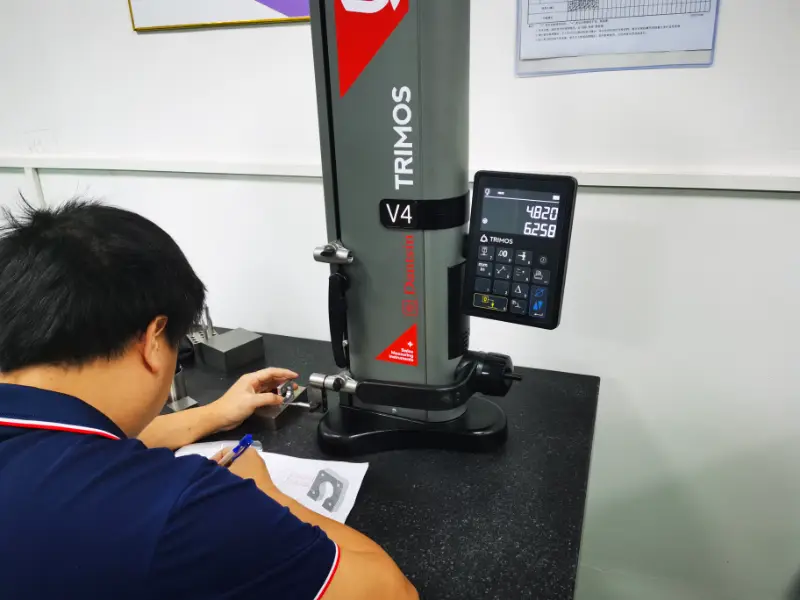
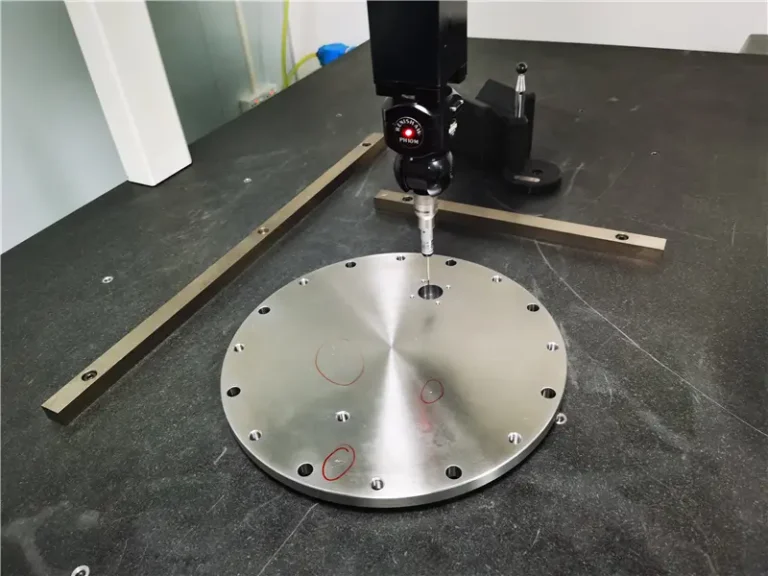
Inspection & release
Measure critical features, clean the part, protect edges, and prepare shipment.